From burrs
to a finished part.
Light deburring after laser cutting, medium and heavy burr removal after plasma or oxy-fuel cutting, grinding, finishing and edge rounding. See how the processing stages differ.
Visual application examples. Configuration, consumables and results are determined for the specific part.
Light burrs.
Clean contours.
Deburring removes fine burrs from external contours and cut-outs. Subsequent edge processing is defined by the part requirements.
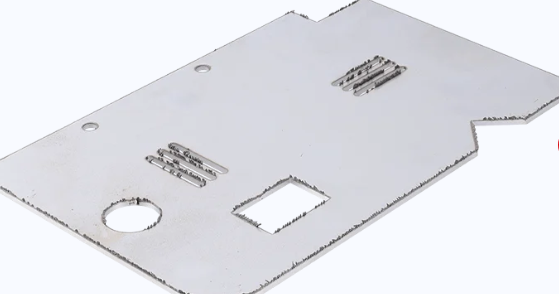
After laser cutting
Light burrs on edges and internal cut-outs.
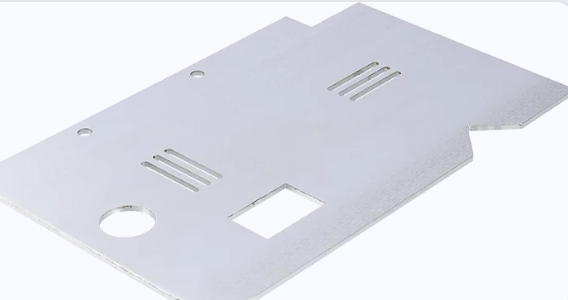
After deburring
Clean contours, ready for the next stages.
Burrs and slag.
Processed edges.
Heavy deposits on thick plate are removed before edge processing. Frames from the NS Máquinas demonstration show the part before and after processing with the DM1100 CC. The choice between CC and DC starts with the actual condition of the part.
Watch the NS Máquinas video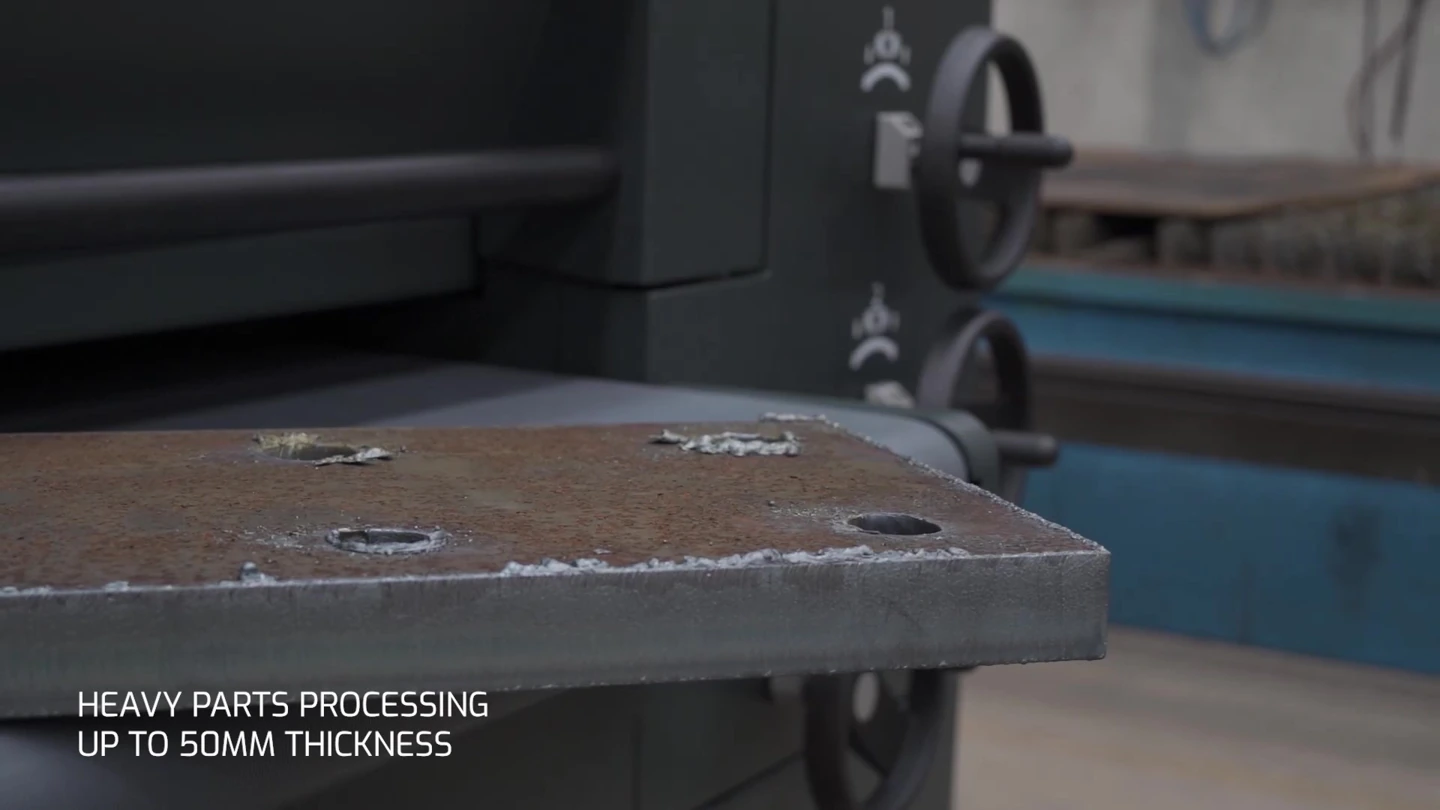
Burrs and slag after cutting
Deposits on the outer contour and inside the holes.
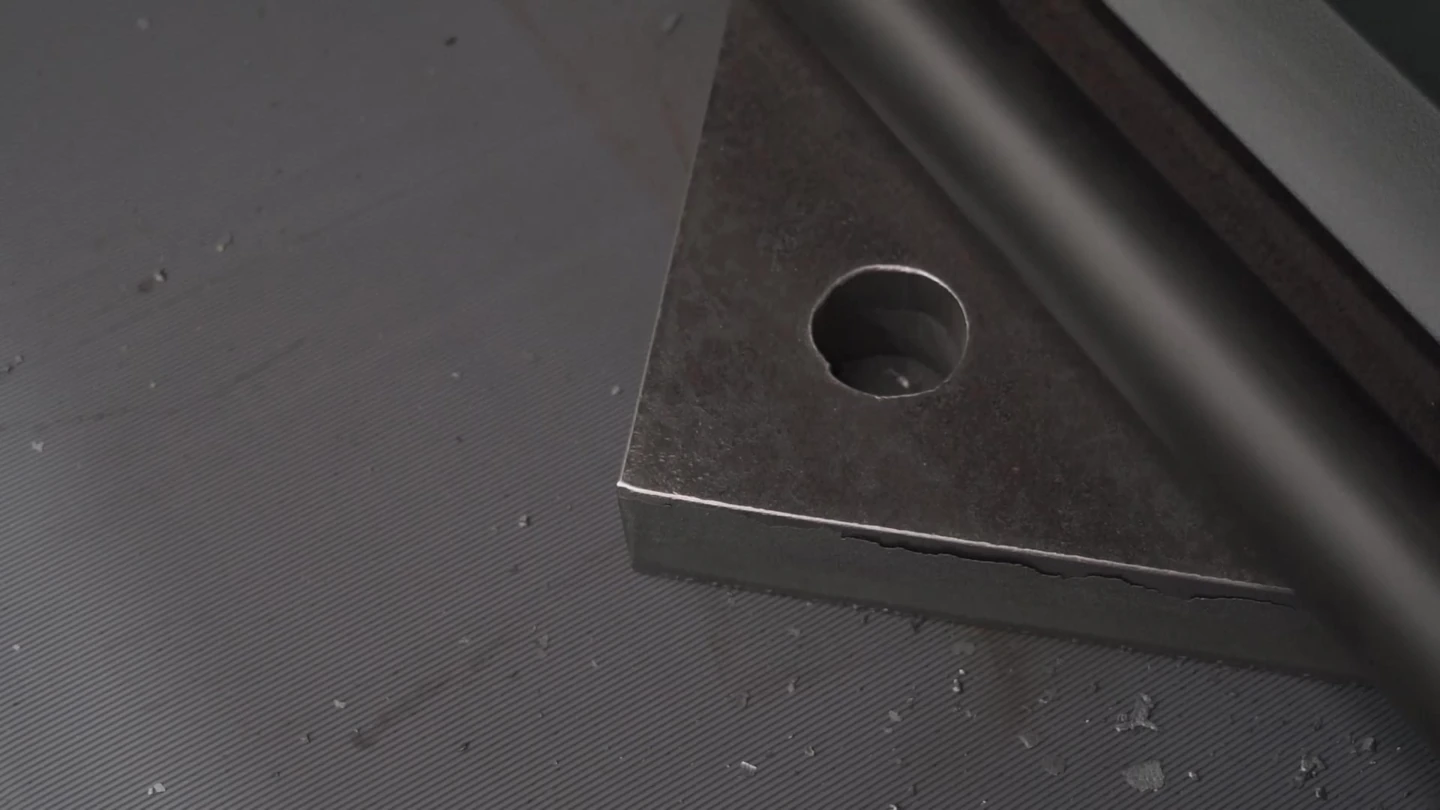
After processing with DM1100 CC
Cleaned edge and processed hole contour.
Grinding and finishing.
The surface finish you need.
After burr removal, abrasive processing produces the finish required by the application. Grit, pressure and feed speed are selected to suit the material and the desired appearance.
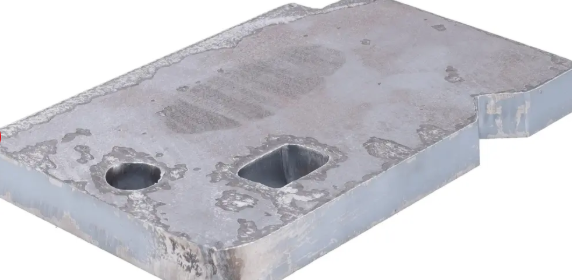
Before grinding and finishing
Example of an unfinished surface with cutting marks.
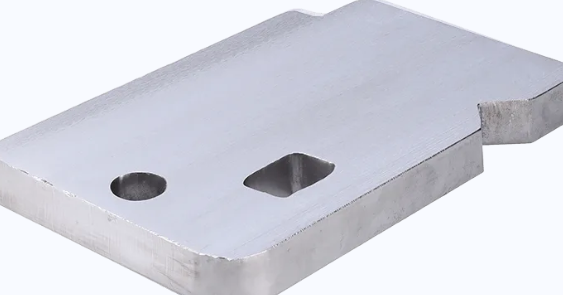
Ground and finished surface
Surface appearance achieved by grinding and finishing.
Edge rounding.
On contours and in cut-outs.
After deburring, external and internal edges can be rounded. The target radius and finish are defined for the part geometry and material.
Before edge rounding
Part with a finished surface, before edge processing.
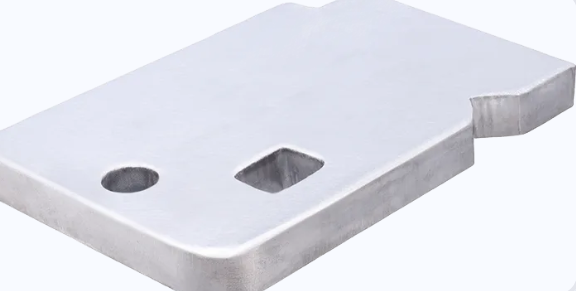
Rounded edges
Visible rounding on the outer contour and internal cut-outs.
Not every part needs
the same stages.
Burr type, material, geometry and finishing requirements define the sequence of operations. Send us your part details to select the machine and configuration.
Discuss your application Compare machines Understand crossbelt technologyWhat to clarify.
Are deburring and edge rounding the same operation?
Deburring removes excess material left after cutting. Edge rounding reduces the sharpness of an edge. Some configurations combine both operations.
Does slag removal also mean surface finishing?
Deposit removal and surface finishing serve different purposes. Depending on the requirements, separate grinding, finishing and rounding stages may be needed.
Can I process any part below the machine’s nominal width?
A width of 1100 or 1600 mm is only one criterion. Thickness, geometry, minimum dimensions, material, burr condition and part support also matter. We confirm the application before configuring the machine.
Can the same radius be guaranteed on every part?
Radius and finish depend on material, geometry, consumables and settings. Include your rounding requirement in the enquiry so it can be checked for your specific application.